
INTRODUCTION
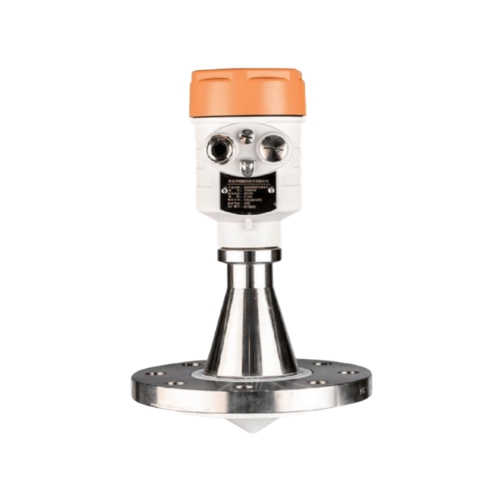
HCDAR-67 Radar Level Sensor Liquid, Slurry, Steam, Condensation Occasions
HCDAR-6x series adopts non-contact measuring method, the output (4-20) mA/RS485 signal, max measuring range is 70m.
The antenna structure is further optimized, and the new microprocessor can perform higher-speed signal analysis and processing.
The instrument can be used in more complicated working conditions such as reactors or solid silos.
WORKING PRINCIPLE
The antenna of HCDAR-6x launches a narrow pulse electromagnetic wave, and electromagnetic wave is reflected back when reach the medium surface and received by the same antenna.
According to the two pulse interval, the microprocessor calculates the distance from the antenna to the surface of the measured medium, and convert it into material level signal.
FEATURE
HCDAR-6x series has small beam angles, and strong anti-interference ability, which improves measurement accuracy and reliability.
The antenna size is smaller, easy to install. It has small measuring blind zone and shorter wavelength.
HCDAR-6X has a good measurement effect for small tanks and small particles. Non-contact measurement, no wear, no pollution.
Output option: 2-wire (4-20 )mA HART and 4-wire RS485 Modbus.
HCDAR-67 Radar Level Sensor Liquid, Slurry, Steam, Condensation Occasions
- HCDAR-61 Radar Level Sensor for Corrosive Liquids
- HCDAR-62 Radar Level Sensor for Liquid & Slurry
- HCDAR-63 Radar Level Sensor for Solid Particle & Powder
- HCDAR-64 Radar Level Sensor for Solid Material & Powder
- HCDAR-65 Radar Level Sensor for River, Reservoir, Lake & Tide Monitoring
- HCDAR-66 Radar Level Sensor for Liquid, Slurry & Dew Resistant
- HCDAR-67 Radar Level Sensor Liquid, Slurry, Steam, Condensation Occasions
HCDAR-67 Radar Level Sensor – High-Precision Level Measurement for Liquid, Slurry, Steam, and Condensation Environments
Advanced Radar Technology for Reliable Industrial Level Monitoring
Accurate level measurement is essential in modern industrial processes. Industries such as chemical manufacturing, power generation, wastewater treatment, oil storage, and food production rely heavily on precise monitoring systems to ensure operational efficiency and safety.
The HCDAR-67 Radar Level Sensor is an advanced industrial instrument designed to deliver high-precision level measurement for liquids, slurry materials, and process tanks operating in environments with steam and condensation. Developed by HCCK, an industrial technology brand of Hebei Huachuang M&C Technology Co., Ltd., the sensor uses high-frequency microwave radar technology to provide stable, non-contact measurement in demanding industrial conditions.
Unlike traditional level measurement technologies that may struggle with vapor, condensation, or fluctuating process conditions, the HCDAR-67 radar level sensor is specifically engineered to maintain consistent performance and measurement accuracy in harsh environments.
With its reliable radar sensing capability, the HCDAR-67 has become an ideal solution for industrial facilities that require continuous monitoring of liquid levels, slurry mixtures, and process fluids.
What is the HCDAR-67 Radar Level Sensor?
The HCDAR-67 Radar Level Sensor is an industrial radar measurement device designed to monitor the level of liquids and slurry materials inside tanks, vessels, and process systems.
The sensor operates using high-frequency radar waves that travel from the sensor to the material surface and reflect back. The sensor calculates the distance between the sensor and the surface based on the signal return time.
This method allows the sensor to provide highly accurate level measurements regardless of environmental interference.
Because radar measurement technology is non-contact, the sensor does not physically interact with the material being measured. This significantly reduces maintenance requirements and increases system reliability.
The HCDAR-67 radar level sensor is particularly effective in environments that include:
-
Steam or vapor inside tanks
-
Condensation on sensor surfaces
-
Turbulent liquid surfaces
-
Thick slurry mixtures
-
Temperature variations
These capabilities make it ideal for industrial process monitoring where conventional sensors may experience limitations.
Key Features of HCDAR-67 Radar Level Sensor
The HCDAR-67 Radar Level Sensor offers a wide range of advanced features designed for industrial reliability and accuracy.
High Precision Radar Measurement Technology
The HCDAR-67 radar level transmitter uses advanced signal processing algorithms to ensure precise level detection in complex industrial environments.
Benefits include:
-
Accurate real-time level monitoring
-
Stable measurement performance
-
Reduced signal interference
This level of precision is essential for industries that depend on reliable process control and inventory monitoring.
Reliable Operation in Steam and Condensation Conditions
Industrial processes often generate steam, vapor, and condensation, which can significantly affect the accuracy of traditional sensors such as ultrasonic or mechanical level devices.
The radar technology used in the HCDAR-67 sensor allows microwave signals to penetrate steam and vapor effectively. As a result, the sensor maintains stable measurement performance even when condensation forms inside tanks or vessels.
Suitable for Liquid and Slurry Applications
Many industrial processes involve both liquids and slurry materials containing suspended particles.
The HCDAR-67 radar level sensor can measure:
-
Industrial liquids
-
Chemical solutions
-
Slurry mixtures
-
Process fluids
-
Wastewater sludge
This versatility makes the sensor suitable for a wide range of industrial applications where material characteristics may vary.
Non-Contact Radar Measurement
The non-contact radar measurement design of the HCDAR-67 sensor eliminates direct contact with the measured material.
Advantages include:
-
Reduced equipment wear
-
Longer operational lifespan
-
Lower maintenance costs
-
Safe operation in corrosive environments
This makes radar sensors one of the most reliable solutions for modern industrial automation systems.
Industrial Applications of HCDAR-67 Radar Level Sensor
The HCDAR-67 Radar Level Sensor is widely used across industries that require accurate monitoring of liquid and slurry levels under challenging process conditions.
Chemical Processing Industry
Chemical production facilities often operate under conditions involving high temperatures, vapor generation, and reactive liquids. The HCDAR-67 radar sensor ensures precise level monitoring of chemical storage tanks and process vessels.
Wastewater Treatment Plants
Wastewater treatment systems contain complex mixtures such as sludge, slurry, and condensation-filled tanks.
Radar level sensors provide reliable measurement without being affected by foam, vapor, or suspended particles.
Power Generation Facilities
Power plants frequently operate with steam and condensate systems that require accurate monitoring.
The HCDAR-67 radar level sensor can measure levels in:
-
Boiler feedwater tanks
-
Condensate tanks
-
Process water storage systems
Food and Beverage Manufacturing
Food production processes often involve liquid ingredients and slurry mixtures.
Non-contact radar measurement ensures hygienic monitoring without contaminating the product.
Pharmaceutical and Biotechnology Industry
Pharmaceutical manufacturing requires precise monitoring of liquid materials under controlled conditions. Radar level sensors provide the reliability and accuracy required for these sensitive processes.
Advantages of Radar Level Sensors Over Other Technologies
Radar level measurement technology offers several advantages compared with conventional measurement methods.
Reliable Performance in Harsh Environments
Radar sensors operate reliably in environments containing:
-
Steam
-
Vapor
-
Foam
-
Condensation
These conditions often cause problems for ultrasonic sensors.
High Measurement Accuracy
Radar signal processing technology ensures highly accurate measurements even when material surfaces are turbulent.
Minimal Maintenance Requirements
Radar sensors contain no moving parts and do not contact the material being measured.
This significantly reduces maintenance requirements and operational downtime.
Long Service Life
Industrial radar sensors are designed for continuous operation over long periods without performance degradation.
Why Choose HCCK Radar Level Sensors?
Industrial companies worldwide rely on HCCK measurement solutions developed by Hebei Huachuang M&C Technology Co., Ltd..
The company specializes in advanced industrial instrumentation and measurement technologies designed for modern automation systems.
Key advantages include:
-
Advanced radar sensing technology
-
Strict manufacturing quality control
-
Reliable industrial performance
-
Durable product design
-
Global supply capabilities
Through continuous research and development, HCCK provides innovative solutions that support the growing demand for industrial process automation and smart monitoring systems.
Installation and System Integration
The HCDAR-67 Radar Level Sensor is designed for easy installation and integration with industrial control systems.
Typical installation locations include:
-
Storage tanks
-
Process vessels
-
Slurry tanks
-
Condensation collection systems
-
Chemical storage containers
The sensor can be connected to plant automation systems to enable real-time level monitoring and automated process management.
Maintenance and Operational Efficiency
One of the most important advantages of radar level sensors is their minimal maintenance requirement.
Because the HCDAR-67 operates using non-contact measurement technology, it is not affected by material buildup or mechanical wear.
Routine maintenance generally involves:
-
Periodic visual inspection
-
System calibration checks
-
Signal verification
This ensures long-term operational efficiency and reduces downtime.
Growing Global Demand for Radar Level Sensors
With the increasing adoption of automation and smart manufacturing systems, radar level measurement technology is becoming the preferred solution for industrial monitoring.
Industries worldwide are shifting toward radar sensors because they offer:
-
Higher accuracy
-
Greater reliability
-
Reduced maintenance costs
-
Compatibility with automated control systems
The HCDAR-67 radar level sensor provides a reliable solution for industries looking to improve process efficiency, safety, and operational control.
Conclusion
The HCDAR-67 Radar Level Sensor is a high-performance industrial measurement solution designed for liquid, slurry, steam, and condensation environments.
By combining advanced radar technology with durable industrial design, the sensor delivers reliable and accurate level monitoring even under challenging process conditions.
Developed by HCCK from Hebei Huachuang M&C Technology Co., Ltd., the HCDAR-67 radar level transmitter is an ideal choice for industries that require precision, reliability, and long-term operational performance.
Whether used in chemical plants, wastewater treatment facilities, power stations, or manufacturing processes, the HCDAR-67 provides the performance needed for modern industrial monitoring systems.


 PT Totalitas Teknik Indonesia
 PT Totalitas Teknik Indonesia
 PT Totalitas Teknik Indonesia

